Transformer radiator powder coating: a plant in Hebei
This Hebei radiator manufacturer runs larger welded assemblies than a typical panel shop: transformer radiators with thick headers and long fins, often over a metre tall and heavy enough that hanger design, not gun count, sets the line.
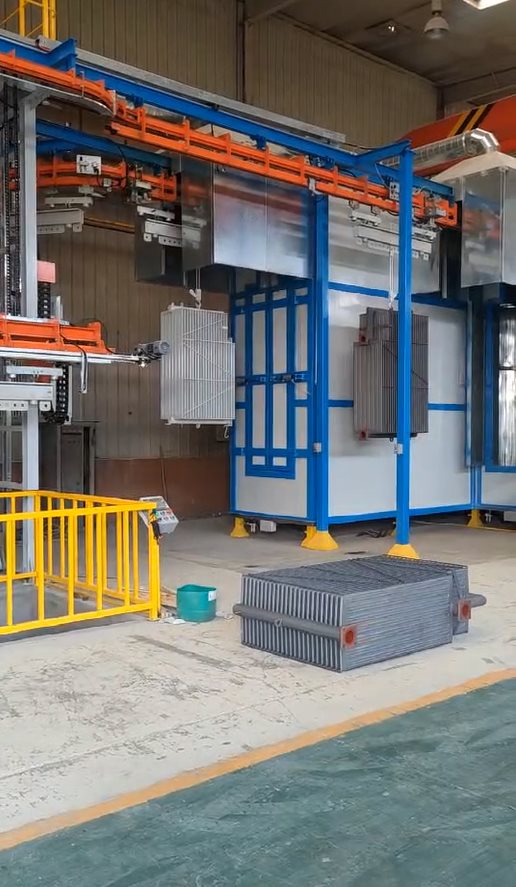
The parts
Large welded transformer radiators: thick header pipes welded to fin packs, single pieces up to about 1,800 mm tall, loaded one or two per hanger.
What the line had to solve
- Hanger load: a standard V-hanger bends under heavy radiators, and a swinging part ruins film uniformity in the oven.
- Core temperature: thick headers need oven dwell long enough to reach cure temperature at the weld, not just at the fin face.
- Load and unload stations have to handle weight safely, which changes conveyor pitch and station layout.
- Powder on header weld seams tends to pull back, leaving a thin band unless the gun angle is set for it.
How the line is built
- Reinforced hangers and a heavier conveyor chain, with pitch set by the tallest and heaviest part rather than average.
- Oven sized on heat-up curve for the heaviest assembly, with a separate hold zone so cure is complete before cooling.
- Gun carriages with an extra pass aimed at header seams, run at a slower line speed than the fin faces need.
- Pretreatment designed for welded parts: degreasing strong enough for weld oil, plus a dry-off that removes moisture from fin gaps before coating.
Acceptance and handover
Specification agreed before signing: film 60-100 um depending on part zone, adhesion class 0-1, oven uniformity +/-5 C at the heaviest part position, and a cure check on a sacrificial test piece cut from the same batch. Handover included load/unload procedure training and a hanger drawing package.
Customer name withheld. Line drawings and the acceptance record can be shared under NDA.
Related
Powder coating line · Powder coating booth · Curing oven · Pretreatment · Watch a radiator line running