PRODUCT LINE
Overhead Chain and Power-and-Free Conveyors
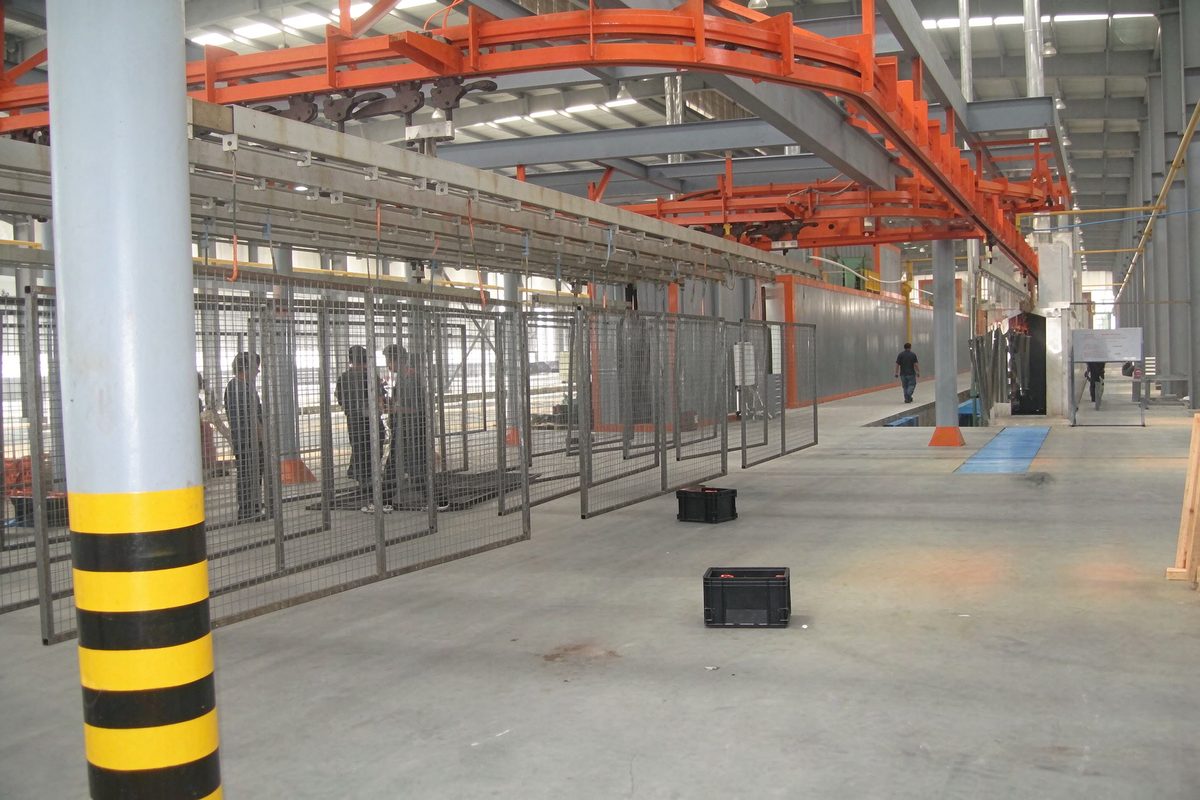
The conveyor ties every station together and sets the takt time of the whole line. We supply overhead chain, power-and-free and floor conveyors, sized to your hanger load, oven temperature and chemical environment.
A simple overhead chain runs continuously at one speed. It is cheap, robust, and right for single-product, high-volume work.
A power-and-free conveyor lets carriers stop at stations independently – essential when pretreatment dips need dwell time while the oven runs continuously, or when you want buffers to absorb a breakdown at one station.
Chain, hangers and lubricators are selected for the environment: stainless or plated parts inside pretreatment and ovens, galvanised chain outside. Variable-frequency drive gives 0.5-6 m/min adjustment.
What is included
- Overhead chain and power-and-free types
- VFD speed control, 0.5 – 6 m/min
- Hanger load typically 50 – 500 kg
- Stainless or plated parts for wet and hot zones
- Automatic lubrication and chain take-up
- Buffers between stations on power-and-free
Typical specifications
| Item | Typical specification |
|---|---|
| Type | overhead chain / power-and-free / floor |
| Speed | 0.5 – 6 m/min, VFD |
| Hanger load | 50 – 500 kg, custom |
| Chain | galvanised or stainless with lubricator |

Not sure which configuration fits your parts?
Send us your workpiece size, coating type and required output per shift. We reply with a line proposal and a budget range within one working day.
Overhead or power-and-free — pick by part flow
The conveyor is the backbone of a coating line: it sets the takt time, carries the hangers through every station, and determines whether you can stop a part in front of a booth.
- Overhead chain conveyor — continuous, simple, lowest cost; parts move at constant speed through all stations
- Power-and-free conveyor — each hanger can stop, accumulate and change speed; essential when parts must dwell in a booth or oven
- Enclosed track — cleaner, keeps lubricant off the parts, common in food-adjacent and high-finish plants
Speed is normally variable from 0.5 to 6 m/min, with hanger pitch set by part size. Chain load, drive power and the number of drives are calculated from your heaviest hanger, not from an assumed average.
What we need to design the conveyor
- Heaviest hanger load and how many hangers on the line at once
- Part envelope, especially height above the hanger
- Which stations need the part to stop (booth, oven, loading)
- Total line length and the hall layout, including any turn
- Whether the line will be extended later
Frequently asked questions
Can we add stations to the line after it is running?
Yes, if we know at the design stage. Extra drive units, turn sections and spare track are added to the original layout so that a second booth or a longer oven can be inserted without replacing the whole conveyor.
How is the conveyor lubricated and maintained?
Enclosed-track conveyors use sealed bearings and need little lubrication; open chain conveyors need periodic oiling at the drive and turns. We supply a maintenance schedule with the drawings, and spare chain links with the shipment.
What happens if the conveyor stops?
The line has an emergency stop that also shuts the guns and holds the oven at temperature. Parts inside the oven can be manually advanced with the hand-wheel or jog function to avoid over-curing.