Powder coating line for street lighting poles
Poles, lamp posts and lighting masts are the hardest shape a coating line has to handle: one piece, several metres long, usually galvanised, and expected to survive ten years outdoors. We build lines for this shape specifically – tall chambers, vertical coating, and a conveyor that can hold a pole still while it is being sprayed.
Why a pole is not just a long part
It is coated whole
A pole is not coated in sections and welded afterwards – the joint would fail first. So pretreatment, booth and oven must accept the finished length, and the conveyor must carry it upright without the tip swaying into a chamber wall.
The surface is usually zinc
Hot-dip galvanised poles need a pretreatment sequence and a powder that behave differently from bare steel: zinc reacts with the chemistry, and a welded pole outgasses at the weld unless the pre-treatment and the heat-up are right.
Thickness matters more than looks
Street furniture is specified by corrosion category, not by gloss. A pole in a coastal or desert-dust environment is a C4-C5 item, which means specified film build, a salt-spray result and edge coverage – not just a colour match.
Output is set by the oven, not the gun
A pole occupies a lot of oven volume for a long time. The number of poles per shift follows from chamber length, carrier spacing and cure time – so the line is sized backwards from the output target.
How the line is laid out
- Load station, by crane. Poles arrive from fabrication or galvanising and are hung vertically on carriers at floor level. The crane envelope defines where the load station can sit.
- Pretreatment, tall spray tunnel. Multi-stage spray with SUS 304 tank walls, labyrinth-jointed and double-welded so stages cannot leak into each other, three-sided sloped bottoms for solution recovery, and nozzles offset ring by ring so a round surface gets no shadow band.
- Dry-off oven. 120-160 °C for 10-15 minutes to drive off moisture before powder – a wet pole is the most common cause of pinholes on a galvanised surface.
- Powder booth with vertical reciprocator. The gun bank strokes the full height of the pole while the carrier holds it still; a pole that drifts while being sprayed gets a thickness wave along its length.
- Curing oven. 180-220 °C for 15-20 minutes with at least 10 minutes at a stable temperature, bridge-type chamber, bottom supply and top return so a 10-metre part is not over-cured at the base and under-cured at the tip.
- Unload, by crane. Cool-down happens on the conveyor; a pole lifted hot will mark.
The conveyor is a power & free system: carriers stop and accumulate independently, so one pole can dwell at the booth or in the oven without holding up the rest of the line. On a pole line this is not a luxury – with a plain overhead chain, every spray stop stops the whole plant.
Typical configuration
| Item | Typical range |
|---|---|
| Pole length | 4 m to 12 m (single piece, vertical) |
| Pole weight | up to 300 kg per carrier, hanger designed per pole section |
| Carrier spacing | 1.2 m to 2.0 m, set by pole diameter and gun stroke |
| Line speed | 0.6 m/min to 2.5 m/min, VFD controlled |
| Pretreatment | 3 to 5 stages, spray, SUS 304, heated by hot water boiler |
| Dry-off / cure | 120-160 °C / 180-220 °C, gas, diesel or electric |
| Film build | 80-120 µm for C4 environments, higher with a zinc-rich primer |
| Output | set by chamber length and cure time – stated per project, not as a catalogue number |
Ranges above are the working envelope we size within; the actual figures for your plant come from your pole list and your output target.
Options that matter on a pole line
- Double coating. Zinc-rich primer plus powder topcoat where the specification is C5 or a coastal site; the line gets a second booth or a flash-off section.
- Two colour families on one line. Two booths on the power & free track, selected by switch, so the plant does not stop for a colour change.
- Automatic gun bank plus manual touch-up at the same station, for brackets and door openings on the pole.
- MES interface and production counting – poles per shift, cure cycles logged per carrier.
- Export packing and site commissioning – modules numbered to a site drawing, engineers on site for assembly and commissioning.
Questions we are asked before an order
Can you coat hot-dip galvanised poles? Yes. Galvanised substrate needs its own pretreatment decision and a powder matched to zinc; we settle that at drawing approval, and we run a trial on your galvanised section before shipment.
What film thickness should we specify? Typically 80-120 µm for a C4 environment, with a salt-spray test to ISO 9227 as the acceptance criterion. If the site is coastal or heavily polluted, the specification moves to a primer plus topcoat rather than a thicker single coat.
How many poles per shift? It follows from oven volume and cure time, not from the gun count. Send us the pole list – the calculation is part of the quotation, and we show you the arithmetic.
Can the same line coat brackets and other parts? Yes, within the carrier and chamber limits. That is one reason we recommend power & free rather than a plain chain: mixed loads can be accumulated and sequenced.
How long is commissioning on site? Typically 2-4 weeks for a line of this size, including assembly supervision, utility checks, oven profiling and a production trial – stated in the contract, not left open.
Reference project
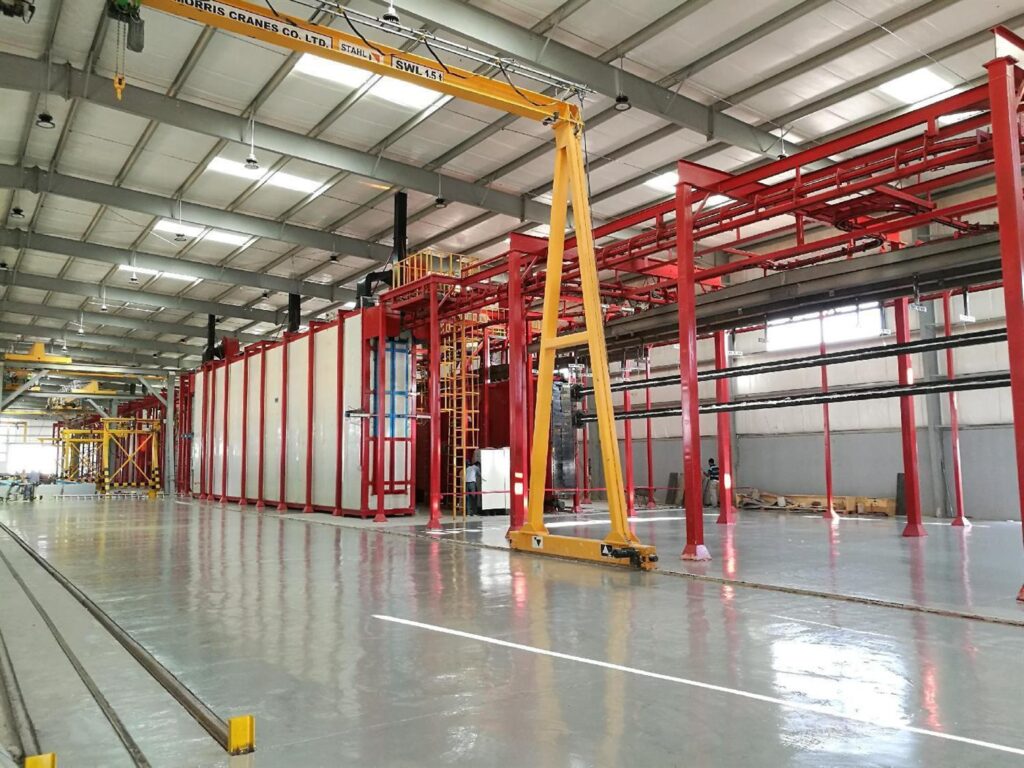
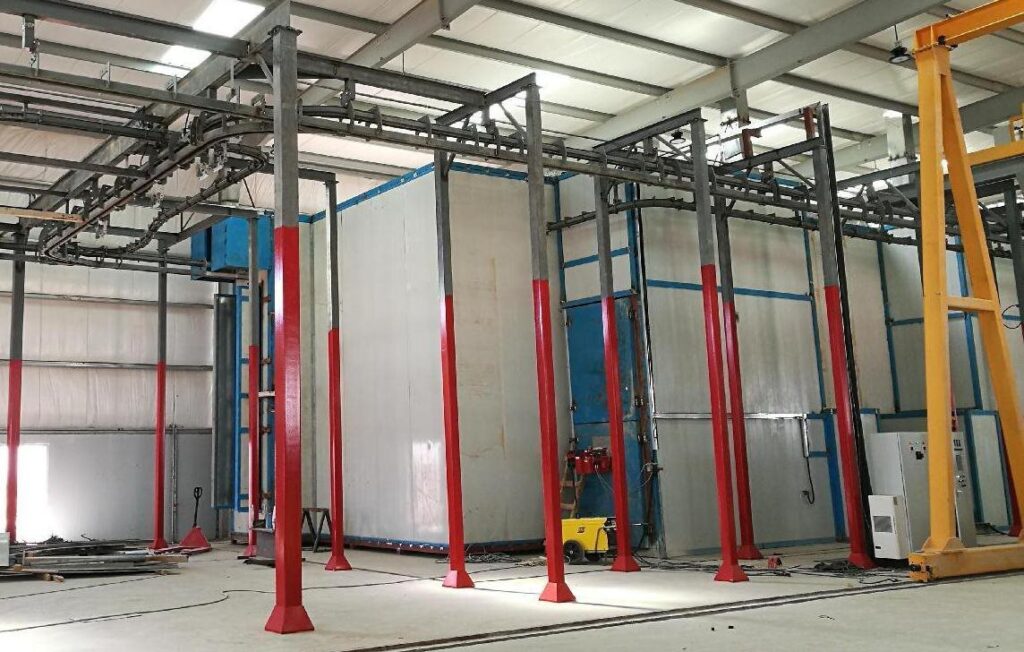
A pole coating line installed in Riyadh, Saudi Arabia: power & free conveyor, rail-mounted frame, tall chambers, built as numbered modules in China and commissioned on site. Read the Riyadh project.
Related: powder coating line, curing ovens, pretreatment, electrical control.