Electrical control system for coating lines
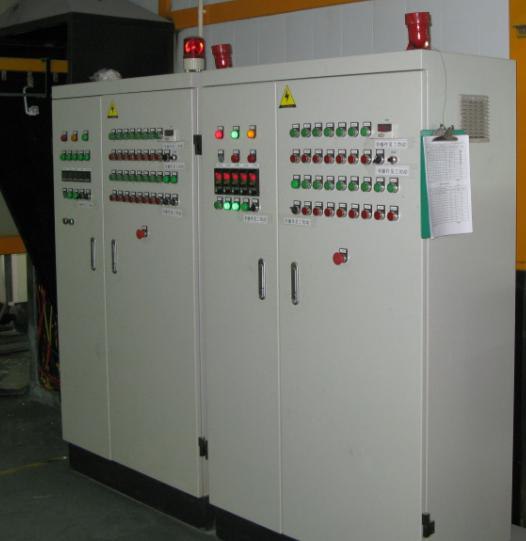
The panel is the part of a coating line that is easiest to cheapen and hardest to live with. Ours is built so that a local electrician, with the drawing set, can find a fault without calling China.
What the system controls
- Conveyor – variable speed drive, start/stop, accumulation logic on power & free lines, jam detection at switches.
- Oven zones – one digital temperature controller and one burner or heater circuit per zone, with high-limit cut-out and fan interlock.
- Booth and recovery – fan start/stop, differential pressure monitoring on filters, recovery unit and powder feed.
- Pretreatment – pump control per stage, bath temperature, level and dosing if the plant specifies it.
- Safety chain – emergency stop at each operating position, gas detection interlocked with the burner, indicator tower per station.
Panel build
- Siemens, Mitsubishi and Schneider for PLC, contactors, breakers and drives – components that can be sourced in most countries, not a proprietary board with a single supplier.
- Touch screen HMI with a line mimic on one page: conveyor speed, zone temperatures, fan and burner status, active alarms, recipe selection.
- One controller per zone, so a zone can be isolated and serviced while the rest of the line keeps running.
- VFDs on conveyor and fans instead of fixed gearbox speeds, which keeps the line adjustable after installation.
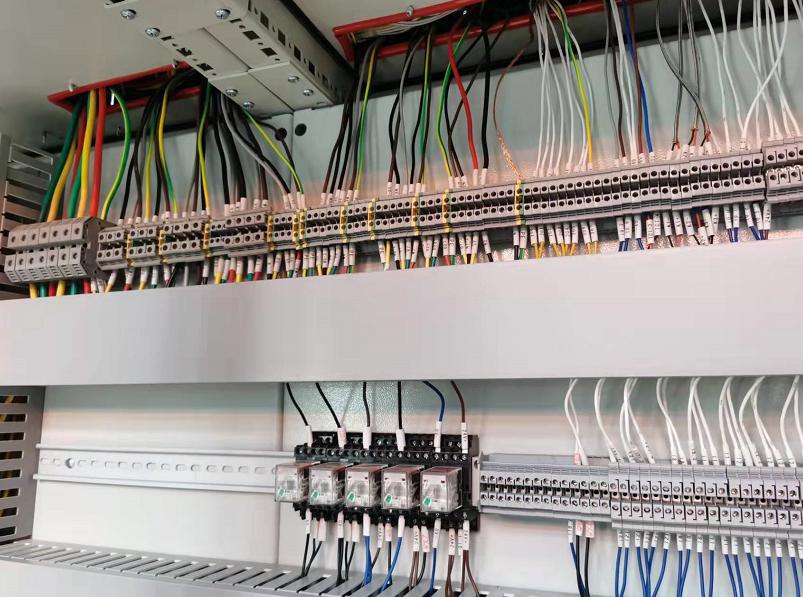
- Separate power and control sections inside the cabinet, with the terminal blocks grouped by function.
- MES interface reserved – terminal position and protocol left ready, so the line can be connected to your production system later without replacing the panel.
Wiring discipline and documentation
Every core in the cabinet is numbered and ferruled, and the numbers match the drawing set delivered with the line. Terminal blocks are grouped by function, power and control are physically separated, and the interior is laid out so a technician can reach a terminal without dismantling half the cabinet. This is the detail that decides what an unplanned stop costs two years from now – not the brand on the breaker.
With the line you receive: electrical schematic, terminal list, PLC I/O list, drive and controller parameter record, and the oven temperature profile charts. Documentation is part of the delivery, not an optional extra.
Options
- Remote support – a router or VPN module so our engineer can read alarms and parameters with your technician on site.
- Energy metering – gas and electricity per zone, useful where the coating line is a cost centre.
- Production reporting – parts counted per shift, cure cycles logged, rejects tagged to a batch.
- SCADA integration – where the plant already runs a supervisory system.
Questions buyers ask
Can we keep spares locally? Yes – the component list is handed over, and the recommended spares (controllers, contactors, a drive, burner control board) are standard catalogue items.
What if our voltage or frequency is different? Panels are built for the site supply (380-415 V 50 Hz, 440 V 60 Hz, 220 V single phase controls) and the drive parameters are set accordingly before the test run.
Who programs the PLC? We do, against the sequence agreed at drawing approval. The program and the I/O list are handed over, and we do not lock the controller.
Related: the full powder coating line, conveyors, and a line built as modules for an export project.