Powder coating lines for tobacco machinery parts
Two projects in the tobacco machinery industry: one power & free powder coating line for a plant in central China and one accumulation conveyor line for a plant in Hunan. Both coat machine frames, covers, guards and stainless sub-assemblies in small batches with frequent model changes.
What the project had to solve
- Small batches, many models. Tobacco machinery is built to order, so the coating line sees frames, covers and guards in low volumes with a high mix of colours and finishes.
- Thick sections and thin covers on the same hanger. A 12 mm welded frame and a 1.5 mm cover cannot be heated at the same rate; if the oven is tuned for the cover, the frame never reaches cure temperature in the core.
- Mixed materials. Carbon steel frames next to stainless and galvanised sub-assemblies, each needing a different pretreatment decision.
- No dust in the finish. These parts are assembled into machines that run in clean rooms, so a dust speck in the coating is a rejected assembly, not a touch-up.
How the line is built
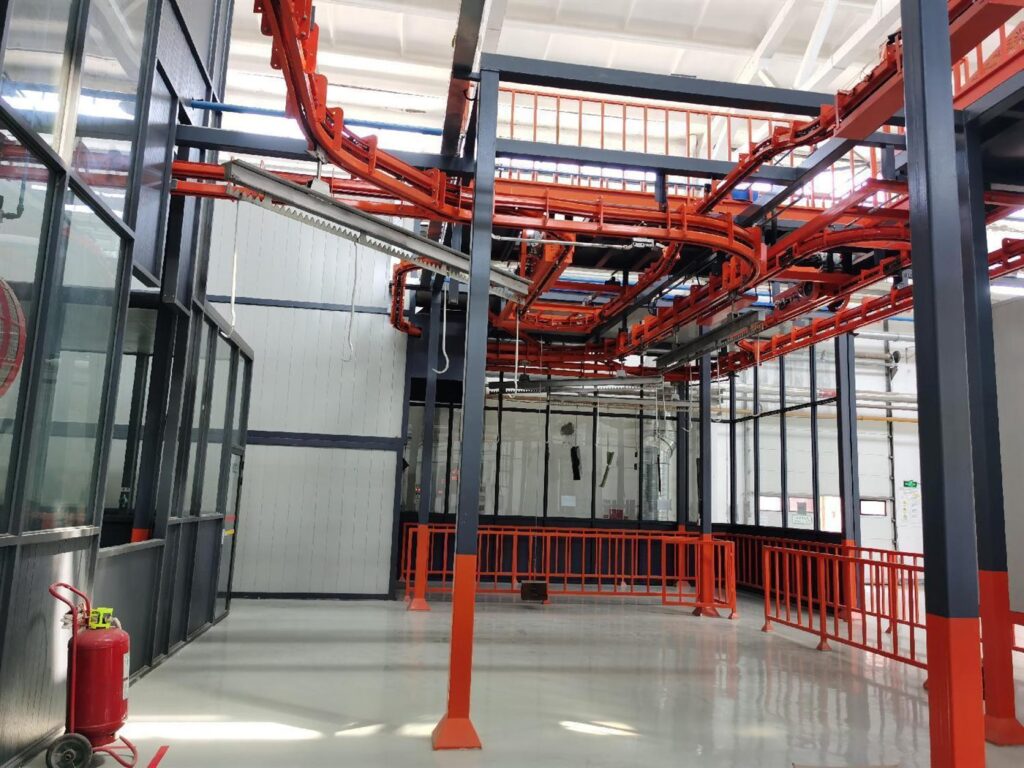
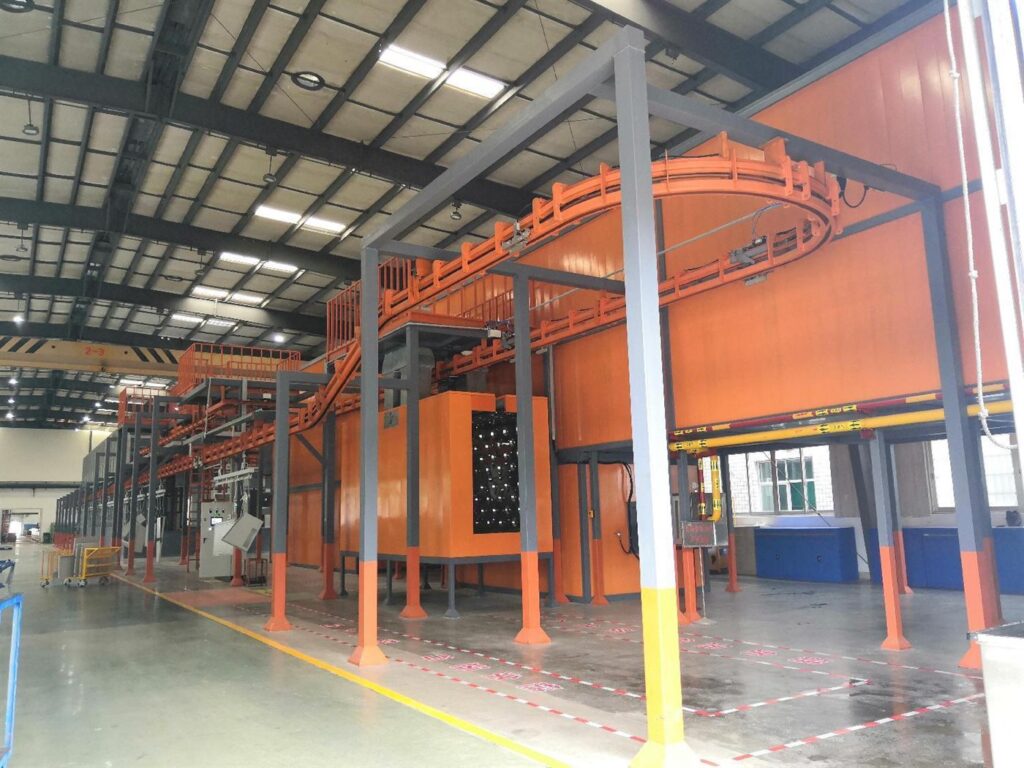
The core of both projects is the power & free conveyor. Its value here is not speed but buffering: carriers accumulate in front of the booth and in front of the ovens, so a heavy frame can stay in the cure zone longer while the light covers behind it wait on the free line. The conveyor also allows route selection at the switches, which is how a mixed-model plant keeps one line instead of two.
Hangers are built per part family: a frame hanger with two support points to avoid distortion during cure, a cover hanger that presents both faces to the guns, and a multi-position hanger for small brackets and labels plates. Load and unload stations are at floor level with a lift assist, and the conveyor carries parts up and over the booth area.
The booth zone is enclosed with tempered glass partitions — dust control matters more than extraction volume on this kind of work. The extraction and recovery system is sized for the powder type in use, and the booth floor is a removable, easily cleaned grating so a colour change does not require scaffolding.
Pretreatment is a multi-stage spray line with SUS 304 inner walls, a galvanised powder-coated outer skin, and a labyrinth joint between tank plates that is welded on both sides. Solution is recovered through a three-sided sloped bottom, nozzles are offset between rings, and heating is by a hot water boiler with a pure water unit for the final rinse — the last rinse quality is what decides whether a powder coat blisters after salt spray.
Curing uses bridge-type chambers with 50 mm rock wool, staggered hand-laid insulation, a static air layer and a folded outer skin. Air is supplied at the bottom and returned at the top with adjustable ducts, giving a flat temperature curve along a part that is 2.5 m long. On the measured profile the same cross-section stays within ±5 °C, which is what keeps a batch of covers the same shade.
Electrical control is a single panel per line: touch screen HMI, one digital temperature controller per zone, variable frequency drives on the fans and the conveyor, and Siemens / Schneider contactors and breakers. Gas detection is interlocked with the burner. An MES interface position is reserved for the plant’s own system.
Acceptance and handover
Both lines were accepted with a temperature profile in each oven zone, a coating trial on three part families (frame, cover, bracket), a cross-cut adhesion test, and a colour comparison against a master sample. The plants ran a full production shift before sign-off, including two colour changes, to check booth cleaning time and conveyor accumulation behaviour.
The takeaway for a buyer
If your parts come in small batches with many models, the conveyor choice matters more than the oven size. Ask any supplier three questions: can carriers accumulate independently, can a single carrier be held longer in the oven without slowing the line, and how long does a colour change take. A line that cannot buffer will always run below its rated output in a high-mix plant.
Coating machine frames and covers? Send us your part families and the number of colour changes per shift, and we will propose the conveyor and booth arrangement.
Customer names withheld at the request of the clients. Photographs are from the installed lines.