PRODUCT
Dipping Type Pretreatment Line
Immersion pretreatment with a travelling hoist and programmed dwell times, reaching inside cavities that spray tunnels cannot.
Tanks are arranged in process order and a travelling hoist lifts the basket through each stage with a programmed dwell: degrease, rinse, conversion coat, rinse, passivate. Parts with box sections, welded flanges and internal cavities get full coverage.
Tank construction follows the chemistry: rubber-lined mild steel for alkaline degreasing, SS304 or PP for acid phosphating and passivation. Electric, gas or steam heating holds stage temperature, and a hot-air drying oven after the final rinse stops water entering the powder booth.
- 3 – 5 tanks with travelling hoist
- PLC programme control for dwell times
- Rubber-lined steel, SS304 or PP tanks
- Electric, gas or steam heating
- Hot-air drying oven after final rinse
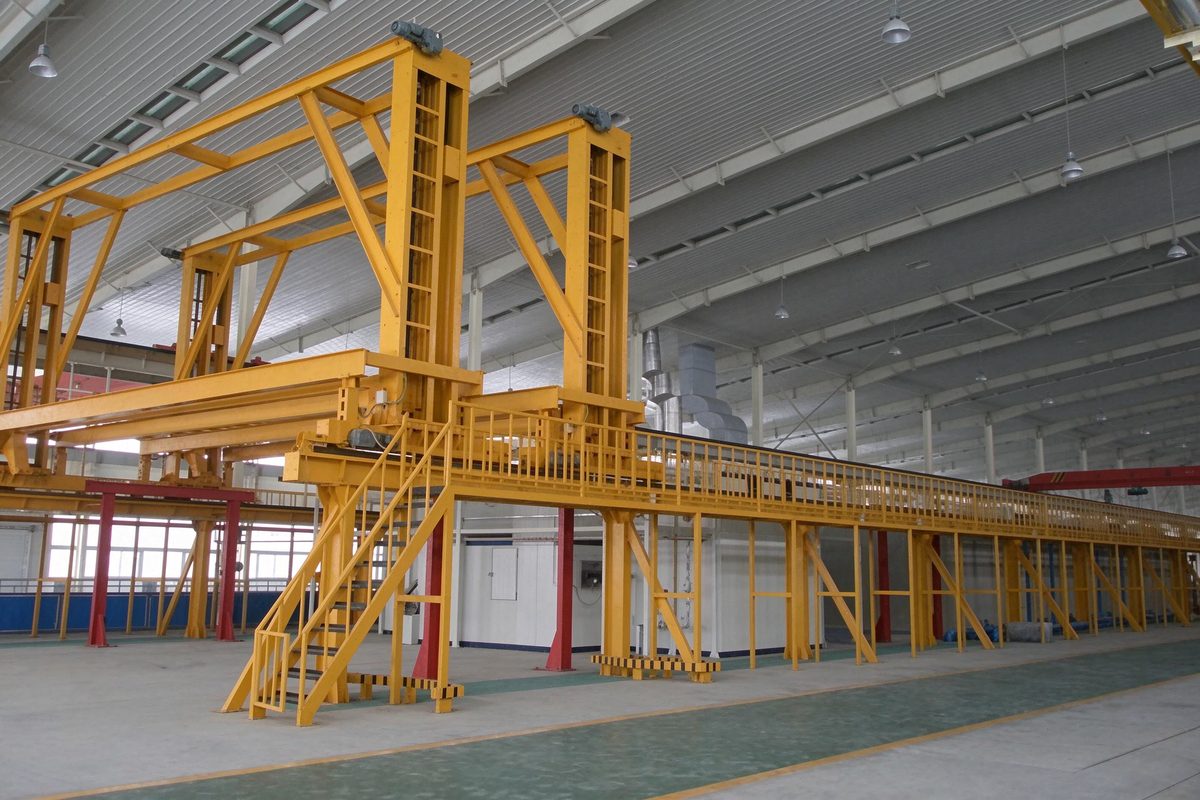


| Item | Typical specification |
|---|---|
| Stages | 3 – 5 |
| Hoist | travelling, PLC programmed |
| Tank material | rubber-lined steel / SS304 / PP |
| Heating | electric / gas / steam |
Not sure which configuration fits your parts?
Send us your workpiece size, coating type and required output per shift. We reply with a line proposal and a budget range within one working day.
Spray pretreatment — when it is the better choice
Spraying uses less chemical and less floor space than dipping, and it heats up faster, so it suits lines that run one shift or change products often. Each stage is a tunnel with nozzles on both sides and a drain back to its own tank, which keeps stages from contaminating each other.
- 3, 4 or 5 stages in one compact frame
- Nozzle spray on both sides with adjustable pressure
- Stage temperatures controlled per tank
- Drain and drag-out design that cuts chemical loss
For parts with deep recesses or hollow sections, spraying can miss areas inside; in that case a dipping stage is added for the critical step, or the sequence is changed to dipping type.